How to Choose Pressure Relief Systems and Their Benefits

Time:2026-10-02 Author:Amelia
0%

Pressure relief systems protect equipment when pressure rises beyond a safe operating range. They may use relief valves, rupture discs, or combined arrangements. In a processing plant, a correctly selected device can prevent vessel damage, production delays, and dangerous releases. Its value becomes clear beside a reactor, compressor, or storage tank operating under changing conditions.

Choosing the right system requires more than matching a valve to a pipe size. Engineers should review operating pressure, temperature, fluid properties, flow capacity, corrosion risks, and possible failure scenarios. Manufacturer data, recognized engineering standards, inspection records, and qualified technical advice provide a stronger basis for decisions. A device that works well with clean air may perform poorly with sticky liquids or corrosive chemicals. Small details matter. Discharge piping, back pressure, maintenance access, and installation orientation can influence real performance.

So, what are the advantages of pressure relief systems? They help limit overpressure, support safer operations, reduce equipment stress, and improve process reliability. They can also lower unplanned downtime when maintained and tested correctly. In practical plant reviews, weak documentation often creates as much uncertainty as weak hardware. That is worth remembering. No selection is perfect, especially when operating conditions change or process data is incomplete. A thoughtful design therefore includes conservative assumptions, clear inspection intervals, and periodic reassessment. The best system is not simply the cheapest or largest option. It is the one that responds predictably, fits the process, and remains verifiable throughout its service life.
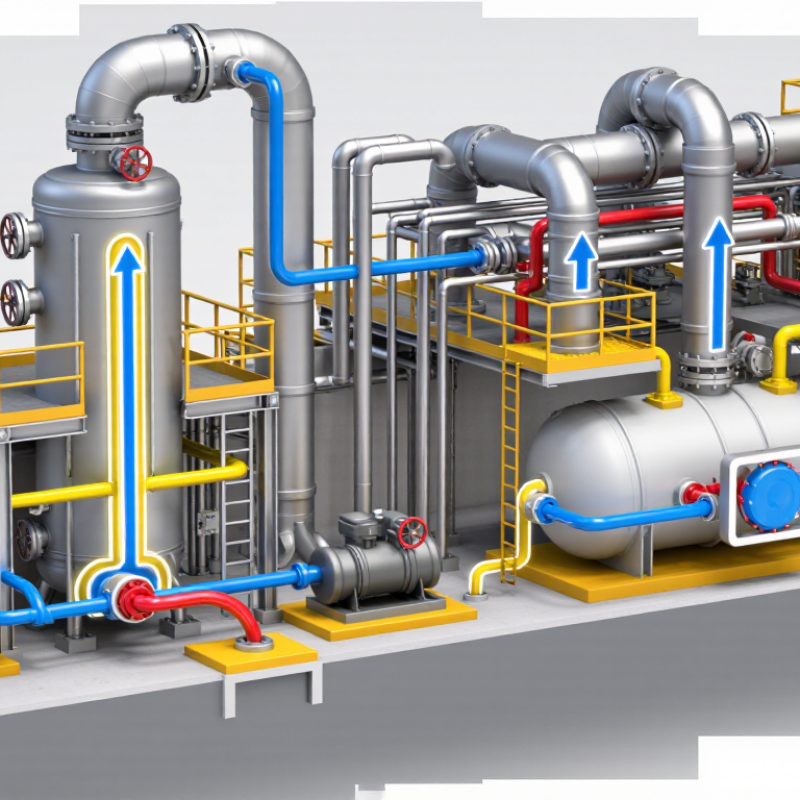
How to Choose Pressure Relief Systems and Their Benefits

Understanding Pressure Relief Systems and Their Purpose

How to Choose Pressure Relief Systems and Their Benefits

Understanding Pressure Relief Systems and Their Purpose

Pressure relief systems protect equipment when pressure rises beyond a safe operating limit. They release excess pressure before vessels, pipes, or reactors lose structural integrity. The purpose is simple. Prevent escalation.

The purpose is simple. Prevent escalation.

A suitable system starts with the pressure source. Thermal expansion, blocked outlets, fire exposure, chemical reaction, and control failure require different relief strategies. Engineers review set pressure, relieving capacity, temperature, fluid composition, and discharge routing. Two-phase flow deserves special attention. It can reduce predictable performance. Corrosion can also weaken a valve before its inspection date.

The U.S. Chemical Safety Board’s 2007 investigation into a Texas City refinery explosion recorded 15 deaths and 180 injuries. That report connected the event to process safety failures, including inadequate hazard control. The figures show why relief protection cannot be treated as a standalone device. It must connect with alarms, shutdown logic, containment, and trained operating teams.

In field reviews, I have seen calculations appear correct while maintenance records remain incomplete. That is an uncomfortable gap. Small details matter. Operators should verify valve accessibility, discharge direction, drainage, isolation controls, and inspection intervals. API 520 and API 521 provide widely used engineering guidance, while OSHA’s process safety requirements support documented hazard analysis. No selection is perfect. A realistic review should question assumptions, especially changing feedstocks, aging equipment, and uncertain relief loads.

Identifying Hazards and Selecting the Right Protection Level

How to Choose Pressure Relief Systems and Their Benefits

Selecting a pressure relief system begins with identifying credible hazards, not choosing equipment from a catalog. Review blocked outlets, thermal expansion, fire exposure, gas generation, and control failure. Process conditions matter too. Temperature, pressure, fluid properties, and corrosion can change the required protection level. A neat calculation is not always a complete answer.

Engineers should define the worst credible scenario and compare it with the vessel’s allowable pressure. Relief devices must respond quickly, discharge safely, and remain maintainable. Consider whether the release needs piping, a vent stack, filtration, or controlled collection. Field inspections often reveal overlooked details, such as closed valves, weak supports, or drains placed too close to walkways. These details can affect both worker safety and system reliability.

Tips: Map every pressure boundary before selecting protection. Confirm operating and design data with process, maintenance, and safety teams. Use recognized engineering standards and have an independent specialist review the design. Avoid assuming that a larger device provides better protection; incorrect sizing can create unstable operation. Document inspection intervals and test results. Leave room for doubt. Even experienced teams can miss a changing process condition. Recheck the assessment after modifications, unusual incidents, or repeated nuisance releases.

Comparing Pressure Relief Devices and Operating Principles

Pressure relief systems protect vessels, pipelines, and process equipment when pressure rises beyond safe limits. The correct device depends on the hazard, fluid, response time, and discharge conditions. International pressure equipment standards, including API 520 and ISO 4126, distinguish between devices that reseat and those that open permanently.

A spring-loaded pressure relief valve opens when system pressure reaches its set point. It can reseat after pressure falls, making it suitable for repeated overpressure events.

A pilot-operated valve uses system pressure to control the opening action. It can provide tighter sealing, but contaminated fluid may affect performance.

A rupture disk responds instantly when its designed burst pressure is reached. It does not reseat.

A vacuum relief valve works differently by admitting air or inert gas when internal pressure becomes too low.

The numbers matter. The U.S. Bureau of Labor Statistics recorded 5,283 fatal occupational injuries in 2023, showing why engineered safeguards deserve careful review. Pressure equipment standards also require capacity calculations, backpressure checks, temperature allowances, and discharge routing.

A relief valve sized only for normal operation may fail during fire exposure or blocked outlet conditions. That is an easy mistake.

Field reviews often reveal another weakness: maintenance records are complete, but actual valve conditions are not. Corrosion, polymer deposits, and incorrect spring settings can change opening behavior.

No selection is perfect. Engineers should compare failure scenarios, inspection access, replacement time, and environmental consequences before approving the final design.

Evaluating Installation, Maintenance, and Performance Requirements

Choosing a pressure relief system starts with the installation environment, not only the vessel design. Confirm inlet and outlet piping, discharge direction, drainage, access, and reaction forces. API Standard 521 identifies fire exposure, blocked outlets, thermal expansion, and utility failure as credible overpressure scenarios. Missing one can invalidate an otherwise careful calculation.

Maintenance requirements deserve equal attention. API Recommended Practice 576 emphasizes inspection, testing, records, and control of isolation devices. A relief valve may look clean while its spring has weakened or its outlet has corroded internally. The U.S. Chemical Safety Board reported 15 deaths and 180 injuries in the Texas City refinery disaster, showing how weak process safeguards can amplify equipment failures. The incident was complex, but it remains a practical warning.

Performance should be checked against real operating conditions. Review set pressure, blowdown, backpressure, temperature, fluid phase, and discharge capacity. Compare test results with the original design basis after every major process change. NFPA 30 guidance also highlights fire exposure and emergency pressure control for flammable-liquid storage. Do not trust a single spreadsheet. Field conditions often disagree with drawings. Small details matter, especially a shortened outlet, a locked isolation valve, or a missing drain. A competent inspection scheme, documented under applicable pressure-equipment rules, provides stronger assurance than routine replacement alone. Trade-offs remain unavoidable: higher capacity can increase reaction loads, noise, and emissions. The final selection should balance protection, maintainability, and verified performance.

Measuring the Safety, Cost, and Compliance Benefits of Proper Selection

How to Choose Pressure Relief Systems and Their Benefits

Proper selection begins with the actual risk, not the equipment catalog. Identify blocked outlets, fire exposure, thermal expansion, chemical reaction, and control failure scenarios. Record the fluid, operating pressure, temperature, phase, and required flow capacity. Small details matter. A wet gas may behave differently from a dry gas during discharge.

A correctly sized relief device can prevent vessel rupture, reduce unplanned shutdowns, and protect nearby workers. The financial benefit is measurable through lower repair costs, reduced production losses, and fewer emergency interventions. However, oversizing is not automatically safer. It may cause unstable operation, leakage, or unnecessary maintenance. Discharge piping also needs careful review. Backpressure, corrosion, vibration, and drainage can change performance after installation.

Compliance depends on traceable decisions. Keep sizing calculations, inspection results, material records, set-pressure certificates, and maintenance dates together. Compare the design with applicable engineering codes and local requirements. A competent engineer should verify assumptions, especially when process conditions change. One weakness remains common: teams sometimes approve a device using old operating data. That shortcut can undermine an otherwise strong safety case. Periodic testing should examine the complete path, including isolation arrangements and discharge routing. Field conditions rarely match drawings perfectly. A valve may be accessible on paper but blocked by insulation or scaffolding. Careful walkdowns expose these gaps before they become costly failures.

How to Choose Pressure Relief Systems and Their Benefits - Measuring the Safety, Cost, and Compliance Benefits of Proper Selection

Relief System Type Typical Protection Duty Common Operating Range Primary Safety Benefit Cost and Maintenance Considerations Key Selection Factors Relevant Compliance Considerations
Spring-Loaded Pressure Relief Valve Protection against overpressure in vessels, piping, boilers, and process equipment. Commonly used from low pressure to high pressure; the exact range depends on valve design, materials, and service. Automatically opens at a defined set pressure and limits pressure to the permitted accumulation specified by the applicable code. Generally reusable after testing; periodic inspection, calibration, seat inspection, and replacement of worn parts may be required. Set pressure, relieving capacity, backpressure, fluid phase, temperature, corrosion, and discharge routing. Confirm design pressure, certified capacity, installation orientation, inlet pressure loss, outlet backpressure, and local inspection requirements.
Pilot-Operated Pressure Relief Valve High-capacity protection where operating pressure is close to the set pressure or where tight shutoff is important. Suitable for many medium- and high-pressure applications, subject to pilot and main-valve limitations. Can provide accurate pressure control, high capacity, and reduced leakage during normal operation. May reduce product loss but has greater control complexity; pilot passages and sensing lines require protection from plugging, freezing, and contamination. Operating-to-set-pressure ratio, minimum pressure for stable operation, backpressure, fluid cleanliness, and remote sensing requirements. Capacity certification and installation requirements must match the governing pressure-equipment code and service conditions.
Rupture Disk Fast, non-reclosing protection for gas, vapor, liquid, explosive, corrosive, or highly contaminated service. Available for vacuum, low-pressure, and high-pressure duties; burst pressure is strongly affected by temperature and manufacturing tolerance. Provides rapid full-opening relief and has no moving parts that can stick or leak through a seat. Usually lower mechanical complexity, but the disk must normally be replaced after activation and may require planned inventory. Burst pressure, operating-to-burst-pressure ratio, temperature, fatigue cycles, vacuum resistance, fragment control, and compatibility. Verify certified burst tolerance, installation direction, temperature rating, allowable backpressure, and whether a combination installation is permitted.
Pressure Relief Valve with Rupture Disk Upstream Protection where the relief valve needs isolation from corrosive, polymerizing, toxic, or fouling process fluids. The combined arrangement must be rated for the vessel pressure, temperature, fluid, and possible space pressure between the devices. Combines non-reclosing rapid protection with a serviceable valve while reducing contamination of the valve seat. Can extend valve service life, but adds components, monitoring requirements, installation complexity, and replacement cost after disk activation. Combination capacity factor, pressure between disk and valve, disk type, telltale monitoring, and discharge compatibility. The complete assembly must be evaluated under the applicable code; blockage or trapped pressure between devices must be addressed.
Vacuum Relief Valve Prevents vessel collapse or deformation caused by cooling, draining, condensation, or blocked-in vapor contraction. Typically applied at very low differential pressures; the required vacuum setting is specific to vessel structural design. Protects atmospheric or low-pressure tanks from external-pressure damage that a conventional pressure valve cannot prevent. Usually simple to maintain, but fouling, freezing, insect screens, and weather exposure can affect performance. Required vacuum capacity, tank design vacuum, venting path, ambient conditions, emissions control, and cleaning requirements. Confirm that vacuum protection is included in the tank design basis and complies with the applicable low-pressure storage-tank standard.
Emergency Vent Protection of low-pressure storage tanks during external fire exposure or other abnormal high-vapor-generation events. Used on atmospheric and low-pressure tanks; emergency flow requirements are determined by tank size, contents, and fire scenario. Provides additional vapor-release capacity when normal tank venting is insufficient. May have low routine operating cost, but inspection access, weather protection, and functional checks are essential. Fire exposure, wetted surface area, vapor properties, tank pressure rating, vent path, and safe discharge location. Fire-case sizing and emergency vent construction should follow the applicable tank and fire-protection requirements.
Pilot-Controlled Depressurization System Rapid pressure reduction during major process upsets, fire exposure, or emergency shutdown scenarios. Applied where the process hazard analysis identifies a need for controlled high-rate depressurization. Can reduce inventory pressure and escalation risk when integrated with detection, isolation, and flare or disposal systems. Higher installed and testing cost; requires dependable power, instrument air or nitrogen, control logic, and safe disposal capacity. Required depressurization time, downstream capacity, control-system reliability, noise, emissions, and hazardous-area design. Requires documented hazard analysis, functional testing, safety-system validation, and compliance with process safety requirements.
Selection and Measurement Notes
  • Relieving capacity should be calculated for credible scenarios such as blocked outlet, control-valve failure, utility failure, thermal expansion, chemical reaction, and external fire exposure.
  • Pressure settings, allowable accumulation, sizing methods, materials, inspection intervals, and discharge arrangements are governed by the applicable jurisdiction and equipment standard.
  • Useful performance measures include successful test rate, relief-device leakage rate, unplanned releases, inspection backlog, replacement frequency, maintenance hours, and documented compliance findings.
  • Typical standards used for design and inspection may include ASME pressure-vessel requirements, API relief-system practices, ISO 4126 requirements, and applicable local pressure-equipment regulations. The governing standard should be confirmed for each installation.

FAQS

What is the main purpose of a pressure relief device?

It protects vessels, pipelines, and process equipment when pressure exceeds safe limits.

How does a spring-loaded relief valve work?

It opens at a defined pressure and can close again after pressure falls.

How does a rupture disk differ from a relief valve?

A rupture disk opens instantly at its designed burst pressure. It does not reseat afterward.

When is a vacuum relief device needed?

It admits air or inert gas when internal pressure becomes dangerously low.

Which scenarios should engineers review before selecting a device?

Review blocked outlets, fire exposure, thermal expansion, chemical reaction, control failure, and utility loss.

What installation details can affect performance?

Check inlet piping, outlet direction, drainage, access, reaction forces, backpressure, and discharge routing.

What maintenance problems commonly remain hidden?

Corrosion, deposits, weakened springs, blocked drains, and incorrect settings may not appear in routine records.

Is a larger relief device always safer?

No. Oversizing may cause unstable operation, leakage, noise, higher reaction forces, and unnecessary maintenance.

What records support compliance and reliable operation?

Keep calculations, inspection results, material records, pressure certificates, test results, and maintenance dates together.

How should performance be checked after process changes?

Recheck pressure, temperature, fluid phase, backpressure, blowdown, capacity, isolation arrangements, and discharge routing.

Conclusion

Pressure relief systems are essential safeguards designed to prevent equipment failure when pressure rises beyond safe operating limits. Choosing the right system begins with understanding the process, identifying potential hazards, and determining the required protection level. Different devices operate in different ways, so selection should consider pressure range, temperature, fluid characteristics, response speed, and compatibility with the equipment. A well-matched solution helps control risks while supporting stable and efficient operations.

When evaluating a pressure relief system, installation conditions, inspection access, maintenance needs, and long-term performance should be considered alongside initial cost. Correct sizing and positioning can improve reliability, reduce downtime, and simplify compliance with applicable safety requirements. Regular testing and maintenance are also important for ensuring continued protection. Overall, what are the advantages of pressure relief systems? They include improved personnel and equipment safety, reduced damage and operational losses, better process continuity, controlled maintenance costs, and stronger confidence that pressure-related hazards are being managed responsibly.
Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......